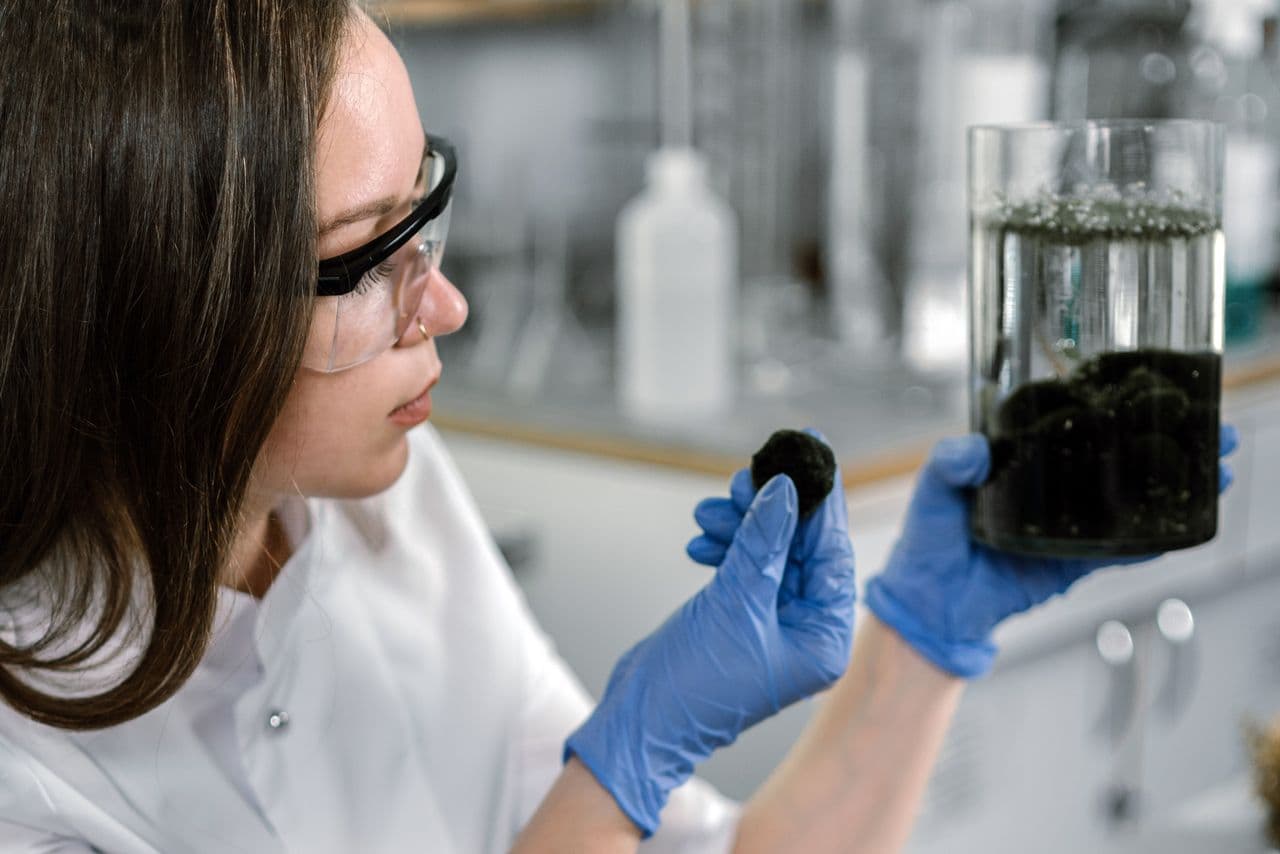
Recover carbon black from polyurethane production waste
 Pimsa Otomotiv A.Ş.
 SKD Türkiye
总结
Polyurethane scrap is pyrolysed into carbon black, formulated into black paint and returned to moulded parts at colour and abrasion performance close to standard.
Context
Submitted through the COP31 Sustainable Transformation Awards · SKD Türkiye (WBCSD Global Network Partner)
Pimsa Otomotiv A.Ş. manufactures polyurethane components for the automotive industry and employs between 251 and 1,000 people.
Moulding polyurethane parts generates production scrap that carries no defect but no route back into the process either. Before the initiative, that scrap was managed as waste and disposed of, mainly through landfill, so the material value embedded in it was written off at the point it left the moulding line.
The company defined the last full production period before implementation as the baseline. In that state, polyurethane offcuts could not be returned to production and were handled purely as a disposal obligation.
The response was to treat the scrap as a feedstock for a pigment the company already buys. Carbon black is the pigment used to colour black polyurethane parts, and it is normally purchased as a virgin material, so recovering it from the company's own waste closes a loop inside a single product family rather than displacing waste into another sector.
The work began in 2025 as a corporate research and development initiative with senior management ownership, and the research and development phase has been completed. The output has been validated on samples and assessed for applicability to production lines that use black paint, but it has not yet been transferred into serial production.
The trials were carried out at the company's research and development centre on its site in the TOSB automotive supply industry specialised organised industrial zone in Kocaeli.
Location of the initiative: TOSB Automotive Supply Industry Specialised Organised Industrial Zone, Kocaeli, Türkiye
Solution
The route has three linked stages, each carried out by the party with the relevant capability.
In the first stage, polyurethane production scrap is processed by thermochemical pyrolysis, carried out with a specialist recycling technology company. Pyrolysis breaks the polymer down in the absence of oxygen and produces three output streams: a solid carbon black fraction, a liquid oil fraction and a gas fraction. Average yields across the trials were 25 per cent solid and between 15 and 20 per cent liquid.
In the second stage, the solid fraction is converted into a functional pigment. Working with a chemicals formulation company, the recovered carbon black was developed into a black paint. The conversion ratio observed was approximately two units of paint for each unit of pigment: 100 grams of recycled carbon black yielded 200 grams of black paint.
In the third stage, the paint returns to the company's own process. It was used at a loading of 4 per cent in polyurethane systems to produce samples, and applied to elastomeric polyurethane vehicle mats, which is a product family where black is the standard finish.
What separates this from conventional polyurethane recovery is the destination. The waste is not downcycled into filler or energy content; it re-enters as a functional pigment with a defined performance specification, which means it has to meet the same colour and wear standards as the purchased material it replaces.
Figure 1: Polyurethane offcuts under pyrolysis in the laboratory tube furnace: the sample in the quartz tube before and after conversion, with the solid fraction that becomes the pigment.


Figure 2: The recovered carbon black powder and the black paint formulated from it, alongside the wear index measured on three samples of the recycled-pigment paint against three standard samples.


Impact
Sustainability impact
Climate
The company states explicitly that the environmental effect has not been calculated as a direct carbon reduction under the GHG Protocol or ISO 14067 at this stage. What has been quantified is the avoided disposal burden.
A baseline scenario was modelled in which 813.75 tonnes of polyurethane waste is sent to an incineration facility. Transport to the facility and the associated disposal processes were calculated to generate 5.216 tonnes of CO2e in total, giving a unit value of approximately 0.00641 tonnes of CO2e per tonne of waste, or 6.41 kg of CO2e per tonne. Converting the waste by pyrolysis instead prevents those transport and disposal emissions from occurring.
These are emissions from waste treatment and transport outside the company's own operations, which places them in Scope 3 rather than in on-site combustion or purchased electricity. The company reports them under Scope 3 Category 5, waste generated in operations, which corresponds to category 4.3 under ISO 14064-1: the waste arises in the company's own manufacturing and, on the conventional route, goes to an external third party for incineration.
The energy side of the substitution has been sized rather than measured. The proposed pyrolysis system would process approximately 100 kg of polyurethane waste a day for an estimated 50 to 80 kWh a day, which at an average solid yield of 25 per cent is an electricity demand of approximately 2.0 to 3.2 kWh per kilogram of recovered carbon black. That electricity is covered by the company's own solar generation, which is fed to the grid and set against the company's consumption.
On an annual polyurethane waste volume of approximately 813.75 tonnes the process could recover approximately 203.4 tonnes of recovered carbon black a year. Taking an indicative cradle-to-gate footprint of 3 to 4 kg CO2e per kilogram for conventional virgin carbon black, the company puts the potential avoidance from that substitution at approximately 610 to 814 tonnes of CO2e a year. The figure is a projection for a system that has not yet been built, not a measured result.
Nature
Polyurethane offcuts that were previously landfilled, and that in the modelled alternative would have been incinerated, are retained as a material instead. Around one quarter of the waste input is recovered as carbon black.
The recovered pigment substitutes purchased carbon black, so the benefit is counted twice in resource terms: waste avoided at the outlet and virgin raw material avoided at the inlet.
Because the route also accepts end-of-life polyurethane parts and not only production scrap, it has a potential application beyond the factory gate, in the product's disposal phase.
Monitoring at this stage is by waste recovery rate, material substitution rate and continuity of product performance, rather than by a certified environmental footprint.
Business impact
Benefits
The clearest commercial benefit is on the disposal side: waste that carried a treatment cost becomes an input, and the volume leaving the site for landfill or incineration falls.
On the purchasing side, the recovered pigment substitutes a bought raw material. Because the conversion produces approximately 200 grams of paint from 100 grams of recycled carbon black, the recovered fraction goes further than a direct one-for-one material replacement would suggest.
Performance parity is what makes the saving usable. Colour values of approximately 24 L, 0 a and -0.4 b under the RAL 9005 standard sit very close to samples made with standard black paint, and abrasion results were effectively identical, so the substitution does not force customer requalification on colour or wear grounds.
No major equipment change is needed on existing production lines, which keeps the adoption cost low for the moulding operation itself.
The company filed a patent application for the technology, and the approach is aligned with the European Green Deal, circular economy policy and emissions regulation, which converts a compliance exposure into a product development asset.
At the current pre-investment stage the recovered carbon black costs the company approximately USD 1.5 per kilogram against approximately USD 2.0 per kilogram for purchased virgin carbon black. On the current disposal rate of approximately TRY 139 per tonne, disposing of 813.75 tonnes of polyurethane waste costs approximately TRY 113,330, which the recovery route would avoid for that volume.
Costs
The cost base is research and development rather than capital plant: pyrolysis trials, paint formulation development, sample production, and the laboratory validation programme covering colour measurement and abrasion testing.
The route depends on two external parties, a pyrolysis technology company and a chemicals formulation company, so the company carries a supply chain dependency for both the conversion step and the pigment step rather than owning the process end to end.
Yields set the ceiling. At an average 25 per cent solid yield, the greater part of the waste input leaves the process as liquid and gas fractions, and only the solid fraction currently has a defined use, so the remaining output streams require their own outlet before the route is fully circular.
The work has been validated at sample scale. Transfer to serial production on lines using black paint is assessed as feasible but has not yet been carried out, so the industrial cost position is not yet established.
Continuity is supported by the patent application, by a planned application to the TÜBİTAK 1832 funding programme and by research and development documentation that keeps the method inside the corporate knowledge base rather than with individuals.
Moving from sample validation to in-house serial production is estimated at approximately USD 130,000 to 145,000 for a pyrolysis system with a capacity of approximately 100 kg a day: approximately USD 115,000 for the reactor and associated equipment, USD 10,000 to 20,000 for the infrastructure and USD 5,000 to 10,000 for environmental permitting and regulatory procedures. The total research and development cost is treated as commercially confidential and is not disclosed.
Impact beyond sustainability and business
Co-benefits
The pigment system is not tied to one part. It can be applied wherever black polyurethane is produced, which extends the potential from vehicle mats to furniture, construction, white goods, footwear and technical polyurethane products.
Because the process accepts end-of-life polyurethane as well as production offcuts, it offers a treatment route for parts returning at the end of the vehicle's life, not only for factory scrap.
The collaboration built technical knowledge across three organisations that would not otherwise share a value chain: a component manufacturer, a pyrolysis operator and a paint formulator. That knowledge base now supports further research and development projects and patent work.
For the manufacturer's customers, a recycled-content pigment raises the sustainable material share of the finished part without changing its appearance or wear behaviour.
Potential side-effects
Pyrolysis is a thermochemical process with its own energy demand, and that demand has not been set against the avoided disposal emissions. Until a full comparison is made, the reported benefit remains the avoided transport and disposal burden rather than a net carbon reduction.
Only the solid output has a defined use. The liquid oil and gas fractions, together roughly 15 to 20 per cent liquid plus the gas share, need their own application or they become a new waste question in place of the old one.
Recovered pigment quality depends on the consistency of the incoming scrap. Polyurethane formulations vary between products, and a mixed or contaminated input is likely to move the colour values away from the tight tolerance the parts require.
The results come from laboratory-scale validation. Yield, colour consistency and abrasion parity at production volumes may differ from the trial figures, and the company treats serial line applicability as an assessment rather than a completed step.
Implementation
Typical business profile
The approach fits manufacturers that mould or extrude polyurethane and generate production scrap of consistent composition on site, particularly those producing parts with a black finish where carbon black is a purchased input.
It is most applicable in automotive component supply, but transfers to furniture, construction products, white goods, footwear and technical polyurethane manufacture, because the constraint is the polymer and the pigment rather than the end product.
The adopting company needs a research and development function able to run formulation and validation work, and access to a pyrolysis operator and a paint formulator, since neither capability is typical inside a moulding business.
Maturity requirement is moderate: existing production lines can use the resulting pigment without major equipment change, so the demanding part is the development programme rather than the plant.
Approach
Quantify and characterise the scrap stream: Establish the annual polyurethane waste volume and its composition, and define the baseline period as the last full production period before any change, so that recovery rates are measured against a real production year.
Model the disposal baseline in emissions terms: Calculate what the waste would generate if sent for incineration, including transport, which in this case produced 5.216 tonnes of CO2e for 813.75 tonnes of waste, or 6.41 kg of CO2e per tonne, giving a defensible avoided-burden figure.
Select a thermochemical pyrolysis route with a specialist operator: Run trials on the actual production scrap rather than on generic polyurethane, and record solid, liquid and gas yields for each trial.
Fix the yield expectation from trial data: Confirm the recoverable fraction before designing the downstream use, which here averaged 25 per cent solid and 15 to 20 per cent liquid.
Convert the solid fraction into a functional pigment with a formulation partner: Develop the paint against the colour standard the parts already have to meet, rather than accepting whatever shade the recovered material produces.
Set the loading level and produce samples: Use the recycled pigment paint at a defined proportion in the polymer system (4 per cent in this case) and produce samples on the same equipment used for standard parts.
Validate colour against the customer standard: Measure Lab values with a laboratory spectrophotometer against the applicable standard, which here gave approximately 24 L, 0 a and -0.4 b under RAL 9005 for the recycled pigment samples.
Validate mechanical performance to a recognised test method: Run Taber abrasion testing to ASTM D4060; here the standard sample fell from 61.51 to 61.26 grams and the recycled sample from 63.72 to 63.45 grams, approximately 0.4 per cent mass loss in both cases.
Secure and industrialise the result: File patent protection, plan a public research funding application, document the method in the research and development portfolio, and assess line-by-line applicability wherever black paint is already used before committing to serial production.
Stakeholders involved
Project leads: The initiative is owned at senior management level as a corporate research and development programme rather than as a technical recycling trial, and is positioned inside the company's objectives on circular economy, carbon footprint reduction and recyclable product range. The research and development and sustainability functions carry project coordination, sample production, testing and validation, which keeps the technical decisions and the environmental objective under the same responsibility.
Company functions: Research and development leads formulation and validation. Quality and laboratory functions run the colour measurement and abrasion testing that determine whether the recycled pigment can be accepted. Production provides the sample runs and assesses which lines using black paint could take the material. Sustainability tracks the recovery and substitution indicators, and documentation is held in the research and development project record so that the method survives beyond the individuals involved.
Main providers: A specialist recycling technology company carried out the thermochemical pyrolysis and the conversion of polyurethane waste into carbon black. A chemicals formulation company developed the black paint from the recovered pigment. The three parties worked through regular technical review meetings at which test results were analysed jointly, and process parameters and product formulations were adjusted in response to the findings rather than fixed at the outset. Each contributed the expertise the others lacked: waste generation and end-use specification, thermochemical conversion, and pigment formulation.
Other: Customer expectations shaped the acceptance criteria directly, particularly on colour standard and mechanical performance, which is why validation was designed around the standards the finished parts already have to meet rather than around a generic recycled-content claim. TÜBİTAK, the national scientific and technological research council, is the intended route for follow-on funding through its 1832 programme, and a patent application secures the method for further development.
Key parameters to consider
Five indicators are tracked: carbon black yield from polyurethane waste, paint yield from the recovered carbon black, colour match against standard paint, mass loss after Taber abrasion, and applicability to serial production lines that use black paint.
Verification methods are mass balance, process yield calculation, product performance testing and quality confirmation. Colour is measured in the Lab colour space with a laboratory spectrophotometer, and abrasion resistance to ASTM D4060.
The environmental effect is currently tracked through waste recovery rate, material substitution and performance continuity. It has not been calculated as a direct carbon reduction under the GHG Protocol or ISO 14067, which is a deliberate statement of scope rather than an omission.
The project started in 2025 and the research and development phase is complete; serial production integration is a stated objective rather than an achieved result.
Implementation and operations tips
Validate against the customer's existing standard, not against a recycled-content target. The reason the result is usable is that colour and abrasion were measured to RAL 9005 and ASTM D4060, the same references the standard part is held to.
Check what happens to the fractions that are not the target output. Only the solid fraction has a defined use here, and any company copying the route should plan an outlet for the liquid and gas streams before scaling.
Split the value chain by capability rather than trying to own it. The moulder does not need a pyrolysis reactor or a paint laboratory; it needs partners who have them and a joint review cycle in which test data changes both the process parameters and the formulation.
Measure the disposal baseline explicitly. Establishing what the waste would have cost in transport and treatment emissions gives the project a defensible environmental figure even before a full life cycle assessment is available.